Skip to content
woodfrog
Industries · Manufacturing

Higher OEE. Fewer defects. Less downtime.

We connect your PLCs, MES and SAP, and show where production, yield and cycle time are leaking, line by line.

Contact usAt least 3× return within 12 months.

Where a typical line loses its time

Illustrative
Planned timeAvailability lossPerformance lossQuality lossOEE

Many plants run near 60% OEE. The gap to 85% hides in downtime, slow cycles and rejects. We make each loss visible by line, shift and machine.

The numbers we move
  • OEEAvailability × Performance × Quality
  • Cycle timeSeconds per part, against takt
  • FPYParts right first time
  • PPMDefects per million
  • MTBFHours between failures
  • MTTRMinutes to repair
  • Scrap %Material thrown away
  • Schedule adherencePlan vs actual output
Problems we fix

Five problems every plant head knows.

Cost figures are common industry numbers, not woodfrog results, unless linked to a case.

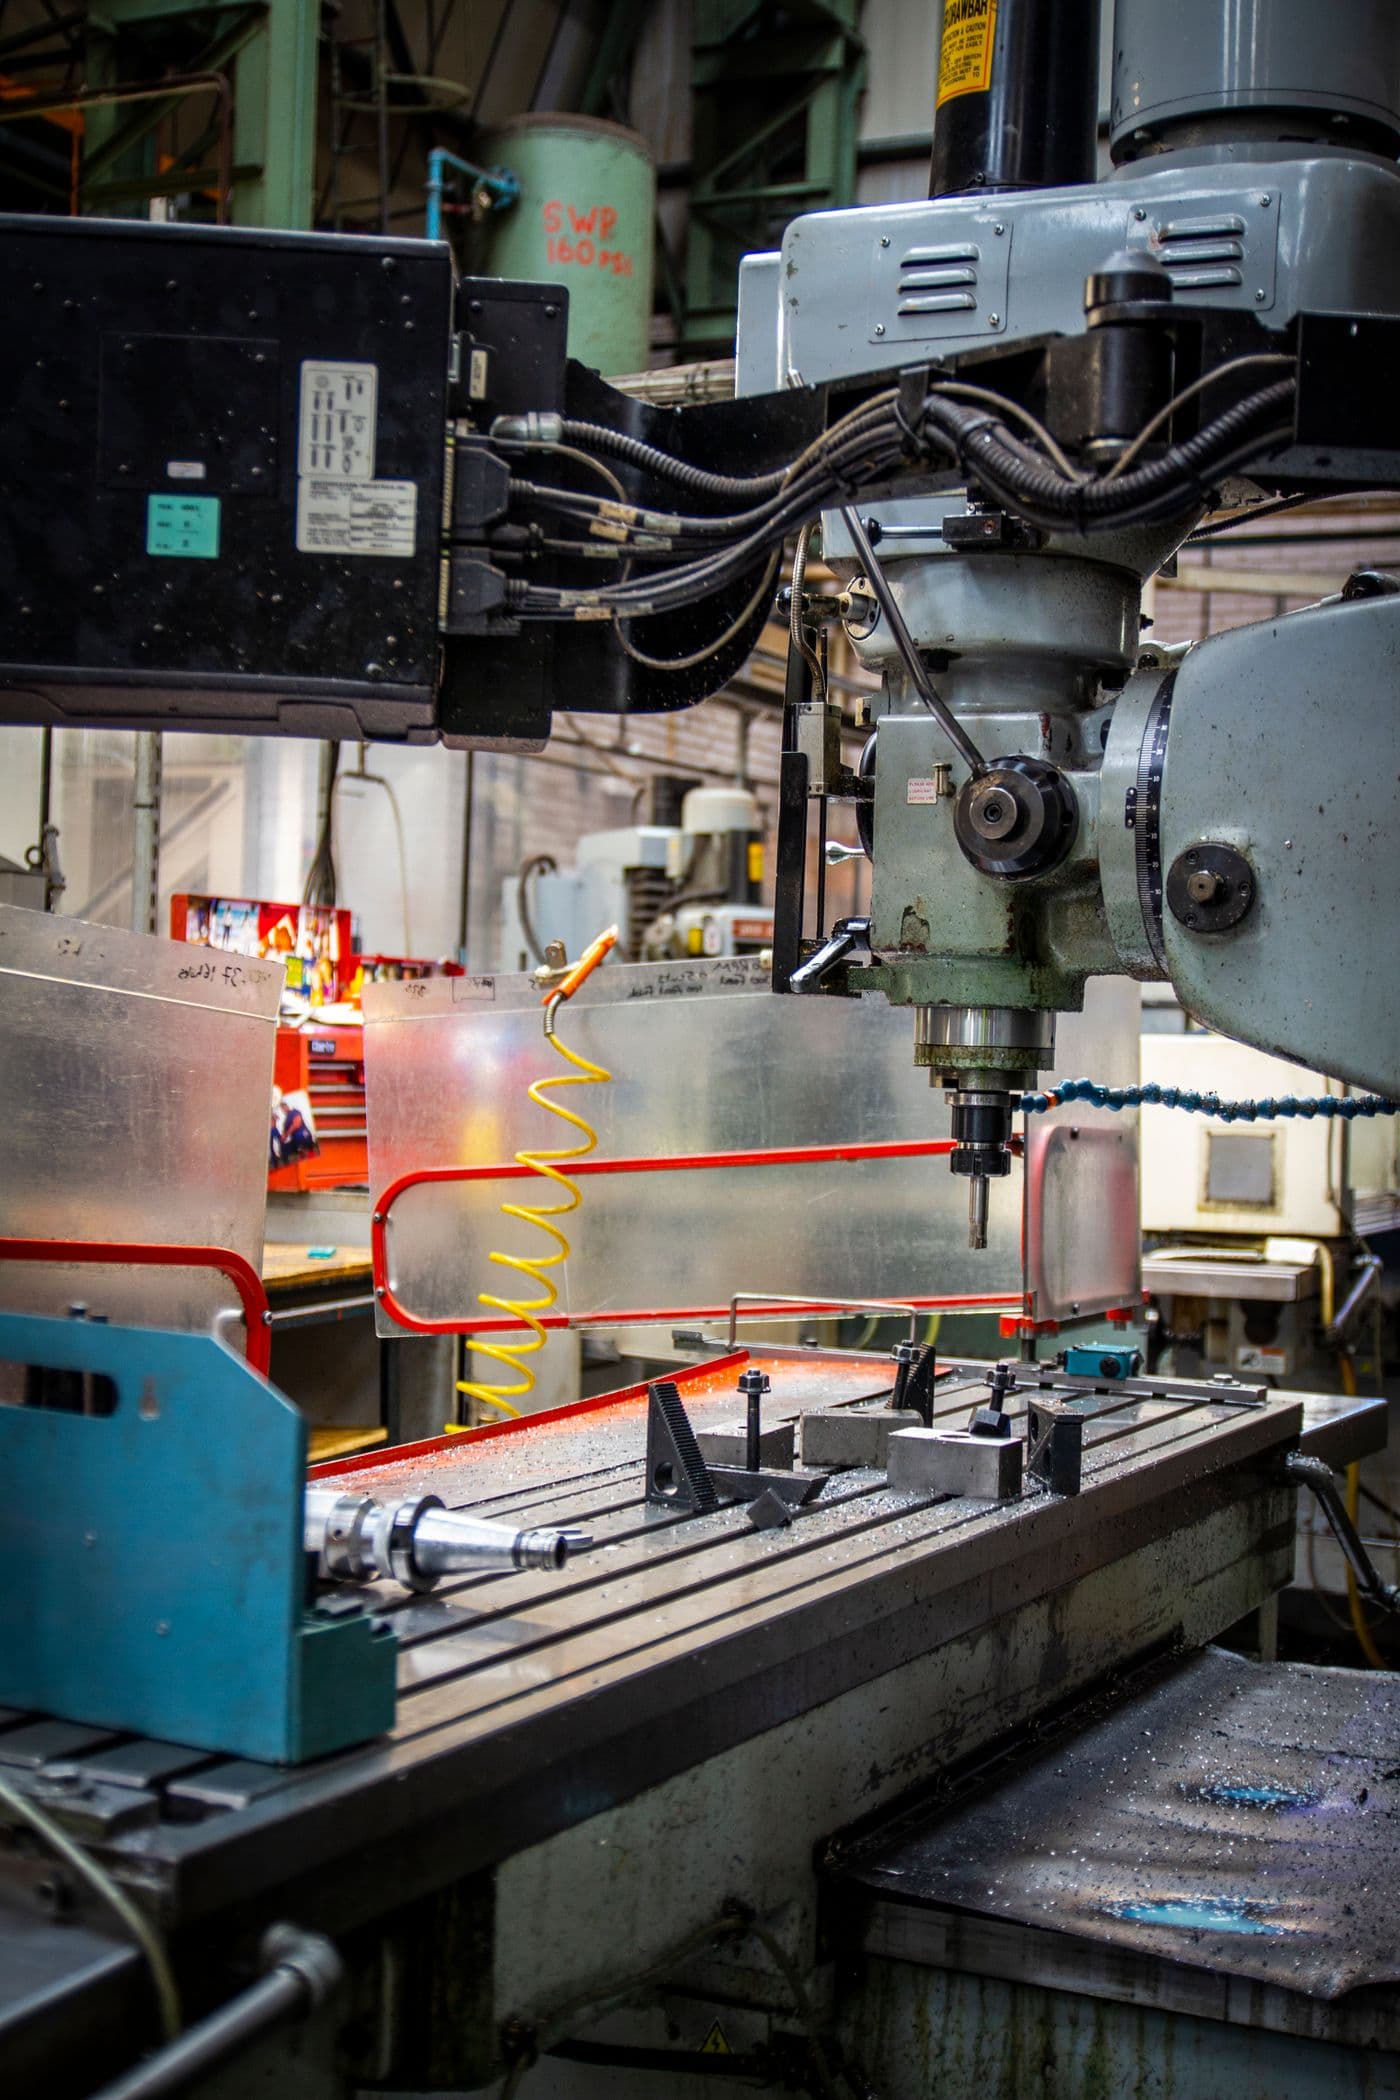
A machining centre on a shop floor
What it costs
~60%common plant OEE
85%world-class benchmark, marked on the bar
01OEE

OEE is stuck around 60%

The daily report averages everything. Nobody sees which machine, shift or loss is dragging the line down.

What we do
DATALive signals from every PLC, no manual logs
ANALYTICSOEE by line, shift and machine, every hour
ANALYTICSSix big losses ranked, so you fix the top one first
DATAPLC · SCADA · MES
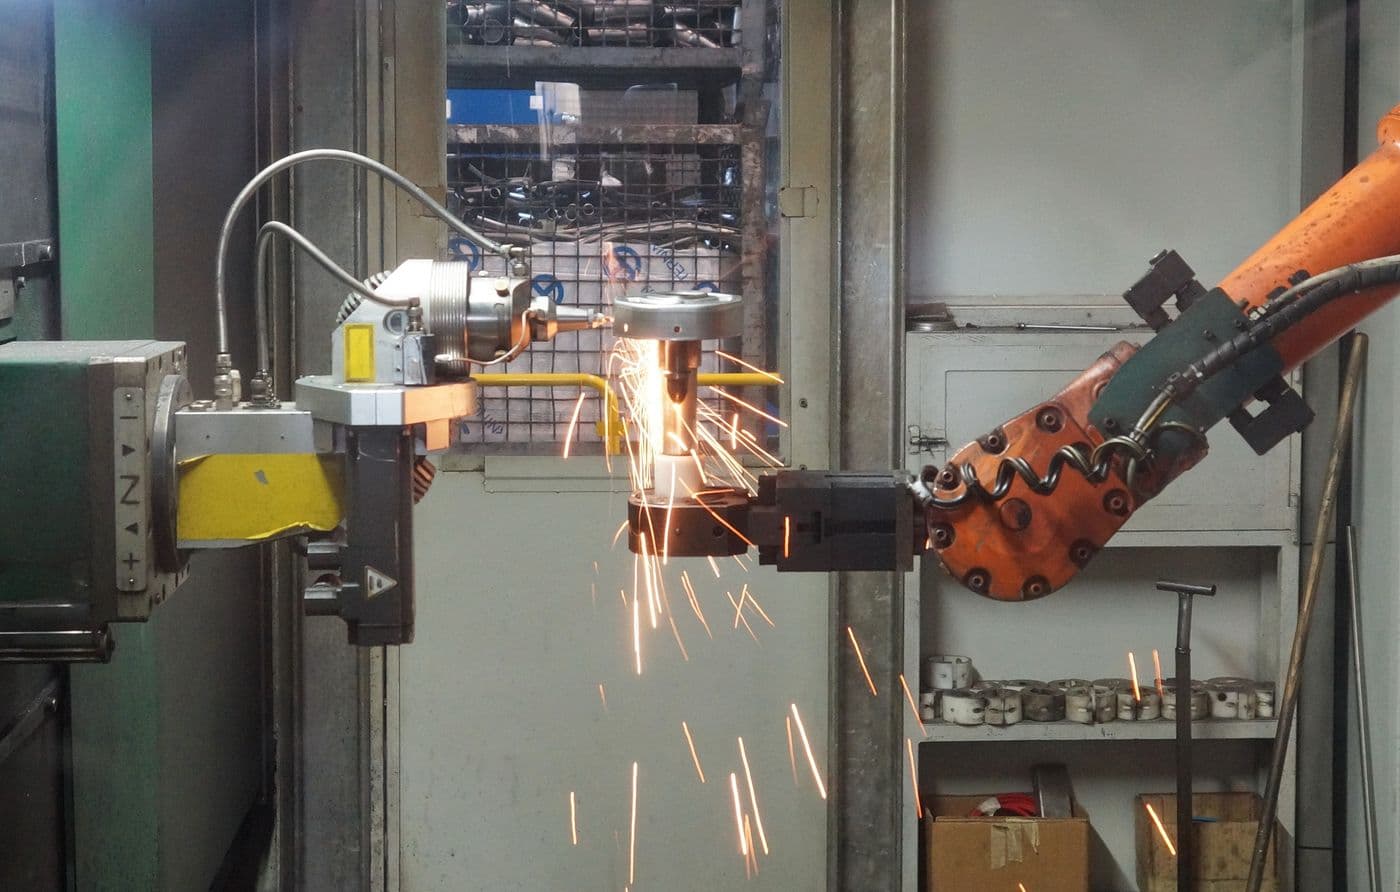
A robot arm welding with sparks flying
What it costs
5–20%of capacity lost to unplanned downtime, commonly cited
Hoursper breakage: scrap, stop, changeover
02MTBF · MTTR

Unplanned downtime and tool breakage

Tools are changed on a count or a guess. Breakdown reasons are typed in after the fact.

What we do
AIEarly warning from spindle load and vibration
ANALYTICSTool life tracked live, per tool
DATADowntime reason codes captured at the machine
Robots assembling a car body in a modern factory
What it costs
15–20%of sales lost to poor quality, commonly cited
1 batchon hold for one failed sample
03FPY · PPM

Defects, scrap and rework

Quality checks a sample and trusts the rest. When yield drops, nobody can say which machine, shift or supplier caused it.

What we do
AIEvery part measured as it is made, alert per part
ANALYTICSDefect root cause by machine, shift and supplier
ANALYTICSFirst-pass yield and PPM on one screen
A yellow industrial robot arm on a production line
What it costs
Secondslost per part add up to shifts per month
1bottleneck station sets the pace of the line
04Cycle time

Cycle time drifts above takt

Cycle time is measured once in a study, then assumed. Bottlenecks move and changeovers run long.

What we do
DATACycle time per station, per part
ANALYTICSBottleneck finder, live against takt
ANALYTICSChangeover time tracked, for SMED
DATAPLC · MES
Process plant stores with tall orange racking
What it costs
0documents retyped with Uloborus
1set of records, indent to invoice
05Plan vs actual

Production plan vs actual

Plan sits in Excel, stock in SAP or Tally, dispatch on paper. Challans and GST invoices are typed twice.

What we do
ANALYTICSSchedule adherence by line and day
DATAStock, batches and orders in one set of records
DATAGST paperwork written from the step that made it
Done before

Already running on real lines.

All case studies →
Systems we connect

From the PLC to the P&L.

Machines
Siemens, Allen-Bradley, Mitsubishi PLCs, CNC controllers
Shop floor
SCADA, MES, historians, IoT gateways, OPC UA
Quality
QC lab systems, CMM, inspection cameras
Business
SAP, Oracle, Tally, Excel

Read only to start. Nothing writes back to the line until you approve it.

PLC · CNC · QCYour plant
Antvia DataOne governed store
OEE · FPY · CycleLive views
Large machinery running inside a factory
Who you work with

Engineers who have stood on the shop floor.

Ananta PatilSamruddhi MoreMandar JoshiParth ManhasPranjul KalsiNarendra P

A small team from Pune, India, close to the Pune and Sangli manufacturing belts. The people who walk your plant are the people who build it.

Meet the team →
Where we have built
Car body shopWeld data captured from welding PLCs, tied to every car.
CNC machiningTool life and breakage signals from spindle load.
Process plantUloborus, built with a contract manufacturer in Sangli MIDC.
Our promise

At least 3x return, within 12 months of delivery.

Measured on your own numbers: OEE, scrap, downtime hours and cost per part.

How we measure it →

Questions plant heads ask.

Do you need new sensors?

Usually not. Most of what we need is already in your PLCs, CNC controllers and MES. Where a signal is missing, we say so in the first audit and suggest the cheapest way to capture it.

Will this disturb production?

No. We start read only, connecting to the data your machines already produce. Nothing writes back to the line until you approve it, and we plan any site work around your shifts.

Our machines are old. Does that matter?

Rarely. Older PLCs and controllers still expose data over standard protocols, or through a small gateway. We have worked with a mix of makes and ages, and the audit tells you what each machine can give.

Can data stay inside the plant?

Yes. The data store can run on your own servers or in your own cloud account, on open formats, so you are never locked in. We work inside your IT and security rules.

How soon do we see OEE live?

The first live OEE view, for the line we start with, typically comes within the first weeks of the build, once the signals are connected. The audit sets the exact plan for your plant.

A plant worker in a hard hat
Tell us your OEE.We will tell you where the next 10 points are.

Talk to us about your plant

Or record your message instead
A person replies within one business day.WhatsApp us